The Impact of Electrical Grounding on Operational Safety and Equipment Lifespan
A grounding system that has been let go is one of the most consistently underestimated failure mechanisms in oil and gas facilities. Unlike a failed pump or a leaking valve, a degraded ground electrode gives you nothing to see until fault current finds a path it should not — through a motor frame, a control panel enclosure, or a worker's body. The fallout runs from nuisance trips that chew into production availability to arc flash events and fires in classified hazardous areas. Getting grounding right is not a commissioning checkbox. It is an ongoing operational discipline.
Why Grounding Matters in Hydrocarbon Facilities
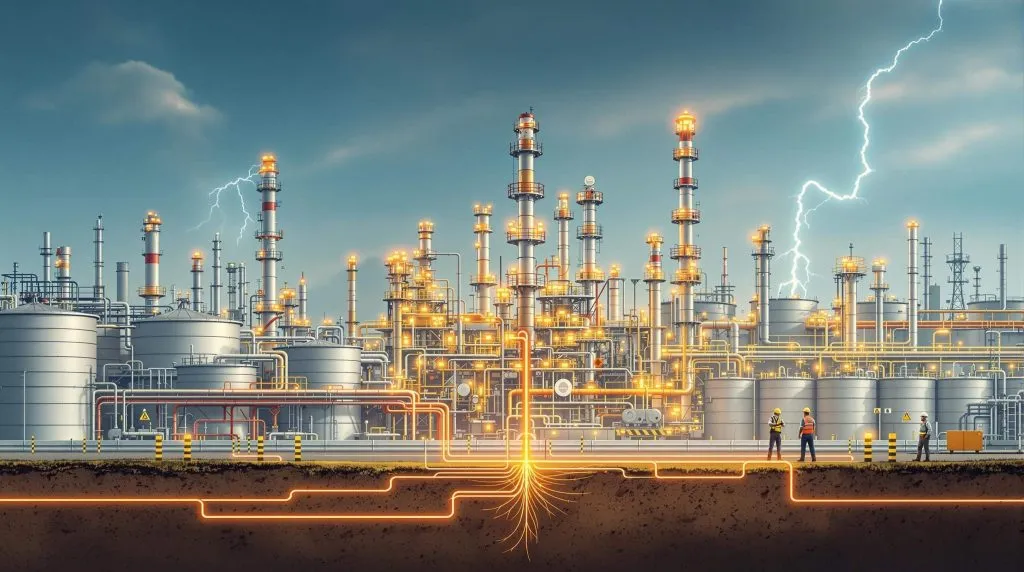
Electrical grounding does two distinct but interdependent jobs. System grounding establishes the voltage reference between the electrical distribution network and earth, controls overvoltages, and defines fault current return paths. Equipment grounding bonds all non-current-carrying metallic parts — motor frames, cable trays, vessel skids, instrument enclosures — to the same reference. That keeps any surface a worker might touch from rising to a dangerous potential under fault conditions.
When either function degrades, the consequences compound. As the Emerson white paper on ground system testing notes, electrical distribution and safety issues caused by poor grounding are well-documented across industrial plants, yet grounding infrastructure is routinely deferred during maintenance planning because it is invisible and its failure mode is gradual.
In a hydrocarbon processing environment, those unintended potentials carry additional risk: an arcing fault in a Zone 1 or Zone 2 area is an ignition source. Grounding is therefore not merely an electrical integrity issue — it is a process safety barrier.
Standards and Regulatory Context
Engineers designing or auditing grounding systems in oil and gas facilities should work within a layered standards framework:
- IEC 60364 (Low-voltage electrical installations) governs system and equipment grounding requirements for the broader electrical installation.
- IEC 61511 (Functional safety — Safety instrumented systems for the process industry sector) requires that the electrical infrastructure supporting safety instrumented functions, including grounding, be maintained to the integrity level demanded by the safety instrumented function.
- NFPA 70 (National Electrical Code) and NFPA 780 (Standard for the Installation of Lightning Protection Systems) set grounding and bonding requirements applicable in North American jurisdictions.
- API RP 505 (Recommended Practice for Prevention of Fires and Explosions in Refineries) addresses bonding and grounding of equipment in flammable atmospheres.
- IEC 60079-14 (Explosive atmospheres — Electrical installations design, selection, and erection) includes specific grounding and bonding requirements for hazardous area equipment.
Where a facility operates across multiple voltage levels — for example, a combined HV substation, MV motor bus, and LV instrument loop installation — the grounding design must account for interactions between those systems. Research on multi-voltage electrical installations confirms that optimising the grounding system across voltage tiers requires explicit modelling of fault current distribution and step/touch potential, not a single-point electrode approach (MDPI, 2024).
Grounding System Architectures
Solidly Grounded Systems
In a solidly grounded system, the transformer neutral is connected directly to earth. This arrangement produces high fault currents on a phase-to-ground fault, which drives fast protective relay operation and limits the duration of the fault. The trade-off is that the high fault current itself can cause mechanical and thermal damage to equipment before the protective device clears the fault.
Solidly grounded systems are common in LV distribution where the NEC or IEC 60364 mandates them, and where rapid fault clearing is preferred over continuity of supply.
High Resistance Grounding
High resistance grounding (HRG) limits ground fault current to a low level — defined by the impedance of the inserted neutral resistor — while allowing the system to continue operating with a single phase-to-ground fault present. This is particularly valuable in continuous process environments where an immediate trip of a motor bus would cause a hazardous process upset. HRG systems increase service continuity and enhance personnel safety by eliminating the arcing ground fault condition that can develop on ungrounded systems (RPM Engineering, 2009).
HRG is applicable to 480 V through 4160 V industrial power systems. A critical operational requirement is that the first ground fault must be located and cleared before a second fault on a different phase develops — a second fault on an HRG system produces a phase-to-phase fault current that the system cannot limit. Facilities using HRG must therefore have a disciplined ground fault location procedure and must not treat the "first fault alarm" as a low-priority notification.
Ungrounded Systems
Ungrounded systems offer similar continuity benefits to HRG but without the controlled fault current limitation. They are susceptible to transient overvoltages that can reach multiples of the nominal phase-to-ground voltage during intermittent ground faults. The Eaton application paper on grounded systems in mission-critical installations identifies overvoltage as a primary driver of insulation degradation and equipment failure in ungrounded systems, and recommends against their use in new installations where alternatives exist.
Comparison of Grounding Architectures
| Characteristic | Solidly Grounded | High Resistance Grounded | Ungrounded |
|---|---|---|---|
| Fault current magnitude | High | Controlled to low level | Low (initially) |
| Continued operation on first fault | No — trips immediately | Yes | Yes |
| Overvoltage exposure | Low | Low | High (transient) |
| Personnel safety on first fault | Dependent on protective device speed | High — fault current limited | Moderate — no current path defined |
| Suitability for hazardous areas | Acceptable with fast clearing | Preferred for continuous process | Not recommended for new installations |
| Maintenance requirement | Periodic relay and electrode testing | Continuous ground fault monitoring mandatory | Periodic insulation resistance testing |
Equipment Lifespan Implications
Grounding quality directly affects the service life of rotating equipment, instrumentation, and power electronics. The mechanisms are several:
Insulation stress from overvoltage. On ungrounded or poorly grounded systems, transient overvoltages stress motor winding insulation cumulatively. Each transient event does not necessarily cause immediate failure, but the insulation system accumulates damage. Over time, this manifests as premature winding failure at a fraction of the motor's design service life.
Stray current corrosion. Where grounding electrodes or bonding conductors are corroded or broken, fault and leakage currents seek alternative metallic paths — pipework, structural steel, instrumentation tubing. Electrochemical corrosion at the point where stray current leaves the metal structure can cause localised wall-loss at a rate disproportionate to general corrosion. In a hydrocarbon piping system, this is a direct integrity threat.
Variable frequency drive (VFD) shaft currents. VFDs produce high-frequency common-mode currents that, without adequate high-frequency bonding between the motor frame and the drive cabinet, circulate through the motor shaft and bearings. The resulting bearing fluting causes premature bearing failure. Proper grounding and shielded cable termination practice is the primary mitigation.
Instrument signal integrity. Ground loops — created when instrument cable shields are grounded at both ends at different potentials — introduce noise into 4–20 mA and low-level thermocouple circuits. In a facility with a degraded grounding system, multiple ground reference points may exist at differing potentials, making systematic ground loop elimination difficult.
The age of a grounding system is itself a risk factor. Ground electrodes, bonding conductors, and clamp connections deteriorate over time; environmental conditions including soil chemistry, moisture, and temperature cycling accelerate degradation (VFC LP, grounding system age article). A system that met its design resistance specification at commissioning may have drifted significantly by mid-facility life.
Illustrative Scenario
The following is illustrative and does not represent a specific documented incident.
Consider a grassroots gas compression station with four MV motor-driven compressors on an ungrounded 4160 V bus. At commissioning, insulation resistance tests on all motor windings pass with comfortable margin. Over several years of operation, transient overvoltages from intermittent ground faults — never alarmed because the system has no ground fault detection — progressively stress the winding insulation. The first winding failure occurs in the third year of operation, attributed to "manufacturing defect." The second failure occurs within the following year. Only when a third motor fails and a root-cause investigation is conducted does the team identify the ungrounded system as the common cause. Retrofitting HRG with continuous ground fault monitoring and replacing the three failed motors represents a cost and schedule impact that a correct initial grounding architecture would have avoided entirely.
Inspection, Testing, and Maintenance Checklist
Ground system maintenance is not a single measurement — it is a programme. The following items define a minimum baseline:
- [ ] Ground electrode resistance testing — Measure and trend electrode resistance at defined intervals using fall-of-potential or stakeless clamp methods. Investigate any sustained upward trend against the commissioning baseline.
- [ ] Bonding conductor continuity — Verify low-resistance continuity from all equipment frames, cable tray, and vessel skids to the main ground bus. Pay particular attention to bolted clamp connections in wet or chemically aggressive environments.
- [ ] Visual inspection of grounding conductors — Check for mechanical damage, corrosion at terminations, and conductor sizing adequacy following any system modification.
- [ ] HRG monitor function test — Where HRG is installed, verify that the ground fault detector and alarm circuit are functional. This test must be performed at a defined frequency; an undetected monitor failure defeats the entire HRG continuity benefit.
- [ ] Insulation resistance trending — Trend motor and transformer winding insulation resistance over time. A sustained downward trend in IR values may indicate overvoltage stress from a grounding system problem rather than moisture ingress.
- [ ] VFD installation audit — Confirm that shielded motor cables are terminated with 360-degree clamp connections at both ends and that motor frames are bonded with a dedicated high-frequency ground conductor.
- [ ] Hazardous area bonding verification — Confirm that all equipment in classified zones is bonded per IEC 60079-14 requirements. Static bonding of road tanker loading points and portable equipment should be on a separate inspection schedule.
- [ ] Post-modification review — Any addition of new equipment, cable rerouting, or substation modification must trigger a grounding review before energisation.
Conclusion
Grounding system integrity is a foundational condition for both personnel safety and equipment reliability in oil and gas operations. Degraded grounding does not announce itself — it erodes insulation life, introduces stray current corrosion, corrupts instrument signals, and creates ignition risk in classified areas, all while appearing electrically normal to operators.
The immediate next step for any facility that cannot produce a recent ground electrode resistance trend, a current bonding continuity record, or a functional test certificate for its HRG monitors is to commission a ground system audit. That audit should cover electrode resistance measurement, bonding conductor inspection, and a review of grounding architecture suitability against the current load configuration — particularly if VFDs or additional MV motors have been added since original commissioning. Treat the findings as you would a pressure vessel inspection report: assign corrective actions, set completion dates, and close them out before the next scheduled turnaround.